 الانتقال إلى المحتوى
For a Japanese factory supplied at 6.6 kV, commercial battery storage should be evaluated as a controlled demand-management asset, not selected solely by its nameplate battery capacity. MegSolid provides energy-storage solutions for commercial and industrial applications, but a factory peak-shaving project must begin with the facility’s measured load, its applicable utility contract, its meter configuration and an engineered connection design. The practical objective is to lower metered site import during the relevant demand interval without creating another maximum-demand event when the battery recharges.
- Separate the required kW of demand reduction from the required kWh of discharge energy.
- Confirm whether a 30-minute maximum-demand calculation applies to the specific meter, contract and utility arrangement.
- Identify the recharge window before deciding that a demand cap is repeatable across production shifts.
- Define the control point, reverse-power-flow requirement and protection boundary with the local EPC and utility-facing electrical engineer.
- Screen named MegSolid systems only against traceable, model-specific technical information.
Confirm the Demand Rule Before Building the Battery Case
A 30-minute maximum-demand approach should be treated as a project assumption requiring local confirmation, not as a universal rule for every Japanese factory. The relevant demand interval, averaging method, billing treatment and consequence of a new peak depend on the applicable supply contract, metering configuration and utility process. Before a commercial battery storage system is sized, the facility should obtain a clear interpretation from the parties responsible for its electricity contract and receiving-power arrangement.
Once that basis is confirmed, the engineering task becomes more precise. The team needs to determine the highest relevant import interval, the intended demand ceiling, the operating margin below that ceiling and the production conditions that produce the peak. This prevents a battery proposal from being based on a single instantaneous load reading that may not represent the metered demand event.
The factory’s own historical data is the primary evidence. The دليل تخزين الطاقة في الحالة الصلبة من C&I can support broader system evaluation, but it does not replace the interval record from the site meter. A useful data set includes the finest available import intervals, production schedules, major equipment starts, shutdown periods and any known abnormal operating days.
Decision Sequence for a Japanese Factory Peak-Shaving BESS
Use this sequence before comparing commercial battery storage options:
- Confirm the applicable maximum-demand rule, meter basis and contract consequence for the site.
- Rebuild the peak-shaving duty from measured import intervals across shifts and worst production days.
- Separate required PCS discharge power (kW) from required discharge energy (kWh).
- Set a contracted-demand ceiling with operating margin, then define who owns the control target.
- Engineer the 6.6 kV connection around the real control point, metering and protection boundary.
- Lock a no-export / reverse-power-flow logic and protect the recharge window as carefully as discharge.
- Screen a named system only after the interval simulation shows the duty can be repeated.
If any step is missing, stop sizing by nameplate battery capacity and complete that step first.
Use Measured Intervals to Identify the Actual Peak-Shaving Duty
A factory can have a high instantaneous motor start, welding event or process transition that attracts attention but does not set the relevant interval demand. In contrast, several moderate loads operating together may remain high long enough to establish a maximum-demand interval. The first analysis should therefore recreate the applicable interval logic from time-aligned site data and show exactly when import exceeded the intended ceiling.
Review more than one operating day. A system that handles a single morning peak may not be able to protect the factory through a second event if there is insufficient time to recharge. Separate the analysis by shift, product mix, seasonal production pattern, planned maintenance state and exceptional days. The design condition should reflect the operational pattern the factory needs to defend, rather than an average day that understates risk.
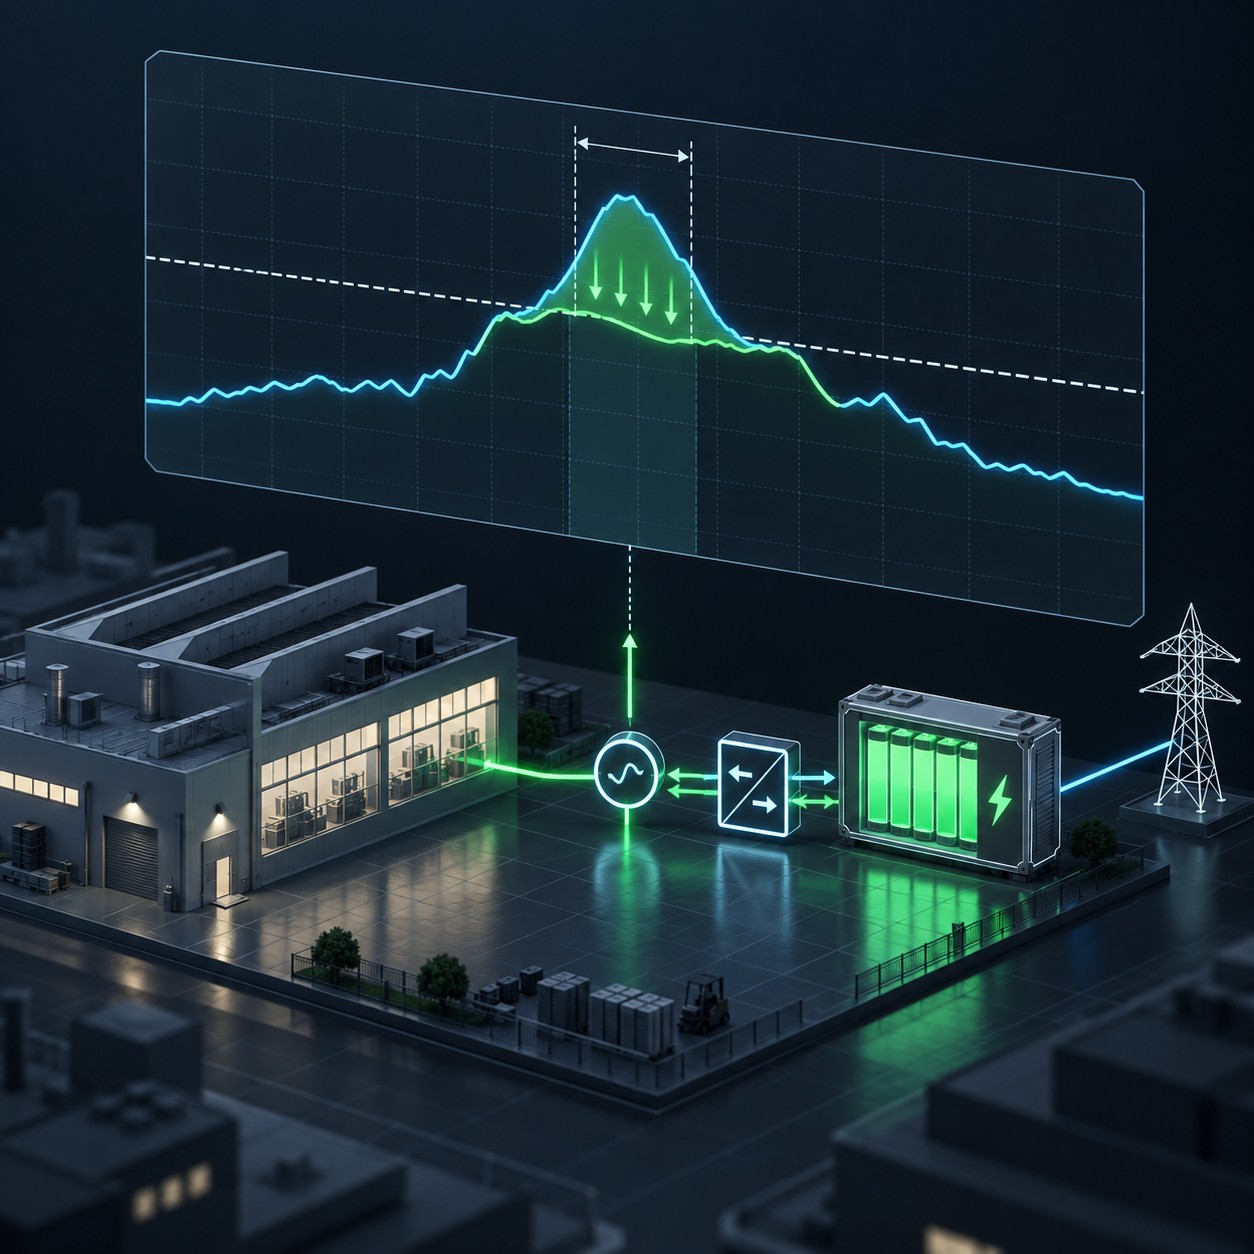
For each relevant interval, identify three values: the original site import, the proposed site-import ceiling and the reduction required from storage. The difference between original import and the target ceiling is the starting point for PCS power. The time for which that reduction must be sustained is the starting point for battery-energy assessment.
Choose PCS Power Before Comparing Battery Capacity
kW is power: it describes how much demand the PCS must reduce at a given moment. If a factory must reduce measured import by 100 kW while the critical event is occurring, the BESS must be able to provide that level of AC discharge under the offered configuration and site conditions. A larger battery-energy figure does not compensate for insufficient PCS power.
kWh is energy: it describes how long the required discharge can be sustained. As an engineering illustration, 100 kW sustained for 30 minutes corresponds to 50 kWh of delivered AC energy. This is a calculation, not a manufacturer rating. Project losses, operating reserve, auxiliary consumption, battery operating limits, repeated peaks and the control strategy must be included before the calculation is used for system selection.
The distinction matters when comparing commercial battery storage options. A system may store enough energy for an extended event but be unable to discharge at the kW level required to cap the factory import. Conversely, a system may have adequate PCS power for a short peak but run out of available energy if the peak extends across multiple intervals or returns before recharge is complete.
| Measured project question | Engineering output | Decision consequence |
|---|---|---|
| How far does import exceed the target ceiling? | Required PCS discharge power in kW | The offered system must supply the needed AC reduction during the event. |
| How long does demand remain above the target? | Required discharge energy in kWh | The battery must sustain dispatch for the relevant interval sequence. |
| How many peaks occur before recovery is possible? | Required energy reserve and dispatch sequence | A one-event calculation may be inadequate for a multi-peak shift. |
| When can charging occur? | Recharge-power limit and permitted schedule | Charging must not establish a replacement demand peak. |
| Can export occur at the connection point? | Metering, controller and protection requirements | Reverse power flow may be restricted or require separate approval. |
Once the required discharge power is known, use it as the first screen—not the battery’s nameplate kWh. If the measured demand reduction stays within about 100 kW and the interval-energy check is still open, a 100 kW / 215.04 kWh-class outdoor C&I cabinet such as MegSolid ESSA0100B-0215 is a practical starting point for comparison. Confirm later with the recharge window, 6.6 kV connection design and multi-peak simulation before treating any model as project-ready.
Set a Contracted-Demand Ceiling With Operating Margin
Contracted demand is a commercial and site-specific issue. The factory should determine the current contract basis, the threshold it intends to protect, the commercial consequence of a new maximum-demand event and the procedure for changing the contracted value. A BESS does not automatically alter the contract; it is a controllable asset that may help the site manage import when the tariff, meter and operating conditions support that use case.
The control target is usually an import ceiling below the threshold the factory wishes to defend. That ceiling should include a prudent margin for meter timing, forecast error, site-load changes and the practical response of the storage control system. A margin that is too narrow can leave the facility exposed when several production loads overlap. A margin that is too conservative can force unnecessary PCS power, battery capacity or curtailment of normal operations.
Define ownership of the target. Facility operations should confirm which production loads are expected to run, while the electrical design team confirms where import is measured and how the controller receives its data. The system integrator should then show, through a dispatch simulation, how the proposed logic responds when demand approaches the ceiling.
Engineer the 6.6 kV Connection Around the Actual Control Point
A 6.6 kV receiving system requires an engineered architecture, not a generic statement that commercial battery storage can simply be connected to the factory. The selected point of connection may be on the low-voltage side of a customer transformer or elsewhere in the facility distribution arrangement. That decision affects metering visibility, transformer loading, losses, protection coordination, equipment boundaries and the controller’s ability to manage total site import.
The one-line diagram should identify the receiving equipment, transformer arrangement, BESS connection point, metering location, CT orientation, isolation devices, protection devices and communications path. It should also identify who owns each control function: the BESS controller, factory energy-management system, site switchgear controls or another approved party. The MegSolid BESS hub provides wider storage context, while the exact 6.6 kV arrangement must be designed for the individual facility.
A local EPC and qualified electrical designer should validate the connection plan against the site equipment and applicable local requirements. This review should occur before finalising a power and energy selection because the electrical architecture can affect the usable operating envelope and the project scope beyond the battery enclosure itself.
Prevent Reverse Power Flow Through Measurement, Logic and Testing
Peak shaving normally seeks to reduce grid import, not export energy. Reverse power flow can arise when BESS discharge exceeds the actual factory load at the control point, when a production load suddenly falls, when metering signals are delayed or when CTs and controller settings are incorrectly configured. The control boundary must therefore be defined before the dispatch mode is approved.
The controller should be designed around measured site load at the agreed location. It also needs a documented response for loss of communications, inconsistent meter values, battery operating boundaries, emergency stop commands and sudden load rejection. Whether export is prohibited, limited or permitted is a site-specific interconnection issue that must be confirmed with the responsible utility-facing parties.
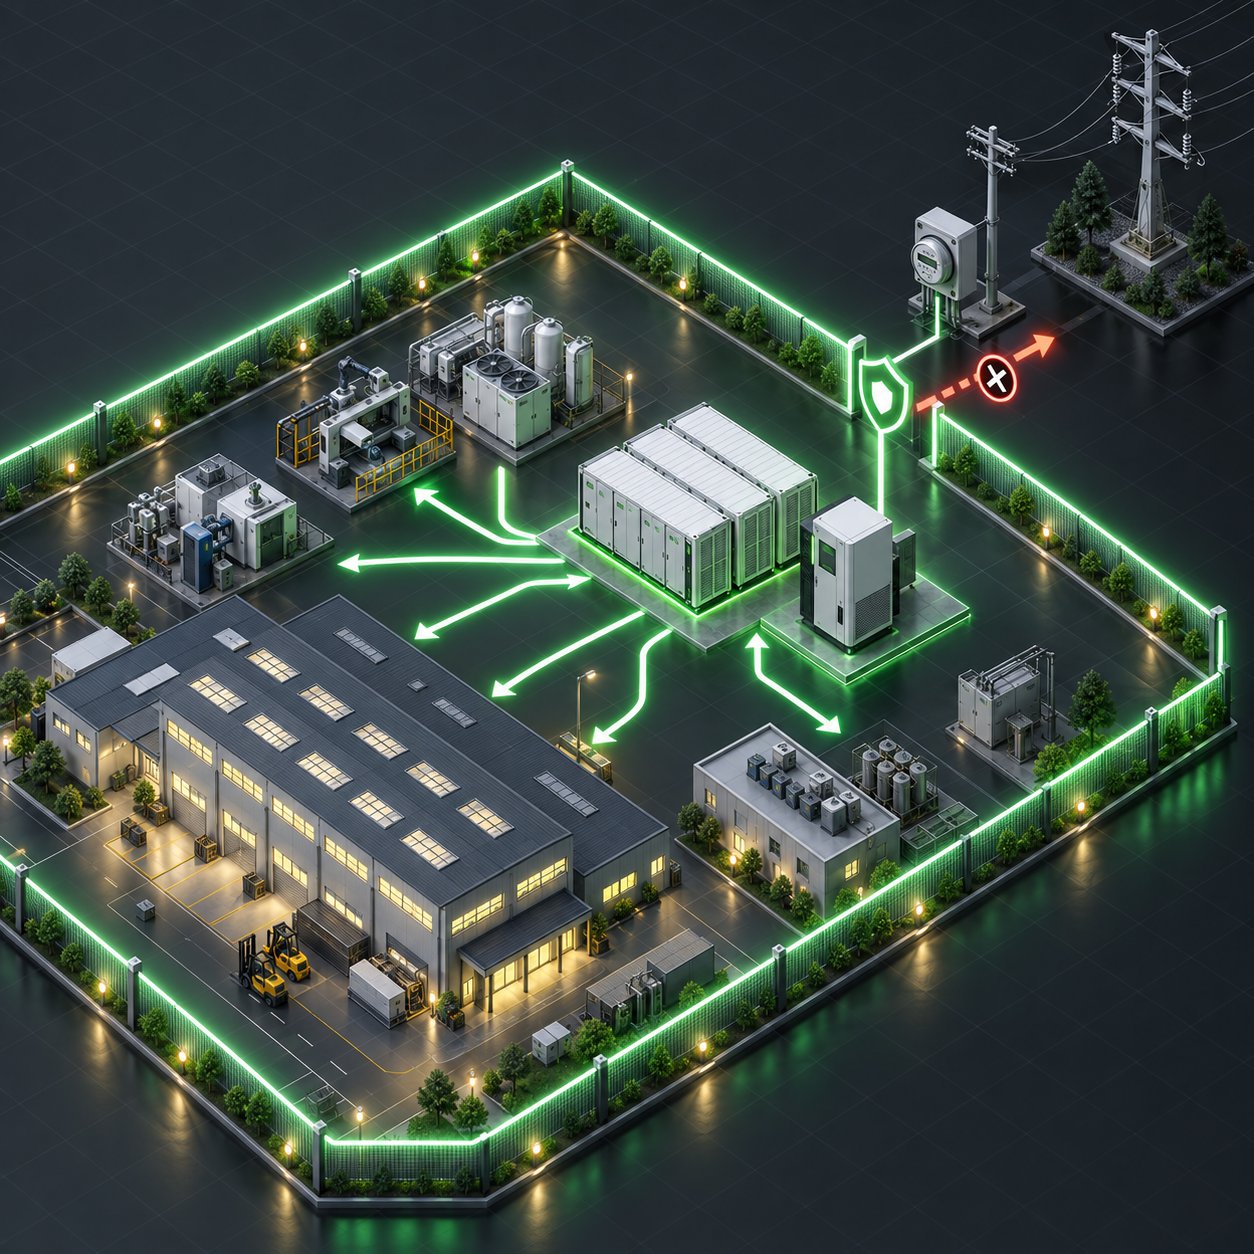
A no-export objective should not be presented as a guarantee of zero export under every possible site transient. Actual behaviour depends on sensor placement, controller response, load dynamics, protection settings and commissioning quality. The commissioning plan should include controlled load-step tests and verification at the relevant meter so that the factory, EPC and utility-facing engineer can assess the agreed acceptance method.
Protect the Recharge Window as Carefully as the Discharge Window
A battery can shave one peak and still compromise the demand objective if it recharges at the wrong time. The recharge window is the period in which the BESS can recover its target state of charge while the combined factory load and battery charging load remain below the selected import ceiling. It is an essential part of the dispatch design, not a secondary operating detail.
For example, a factory may experience lower demand during a lunch period before a later production ramp. Charging may be possible during that lower-load period only if the resulting grid import remains within the demand-control target. If charging continues into the next production ramp, the battery can add to site import precisely when it should be preserving headroom for another peak.
The dispatch strategy should specify a target state of charge before each expected peak, a maximum recharge power, an import guardrail and an exception rule for unusual production days. The MegSolid resource center و BESS news and insights provide supporting technical and market context, but the factory’s own load history must demonstrate whether the recharge plan is repeatable.
Screen Named Systems Against Traceable Ratings Only
Named MegSolid systems are not interchangeable ratings. Screen a model only when the offered configuration is backed by model-specific power, energy and operating data. For this article, ESSA0100B-0215 is the worked example because its listed AC power and nominal energy can be checked against a measured peak-shaving duty.
| Named system | Traceable screening basis | When it can enter shortlisting |
|---|---|---|
| ESSA0100B-0215 | 100 kW rated AC power; 215.04 kWh nominal capacity; 672–850 V battery range | Conditional candidate when required demand reduction stays within 100 kW and the interval simulation supports energy, reserve and recharge |
| Higher-power / higher-energy cabinet or container options | Use only the datasheet and BOM for the exact offered configuration | Compare after the site duty exceeds the 100 kW class, or when cooling, duration or connection design requires another architecture |
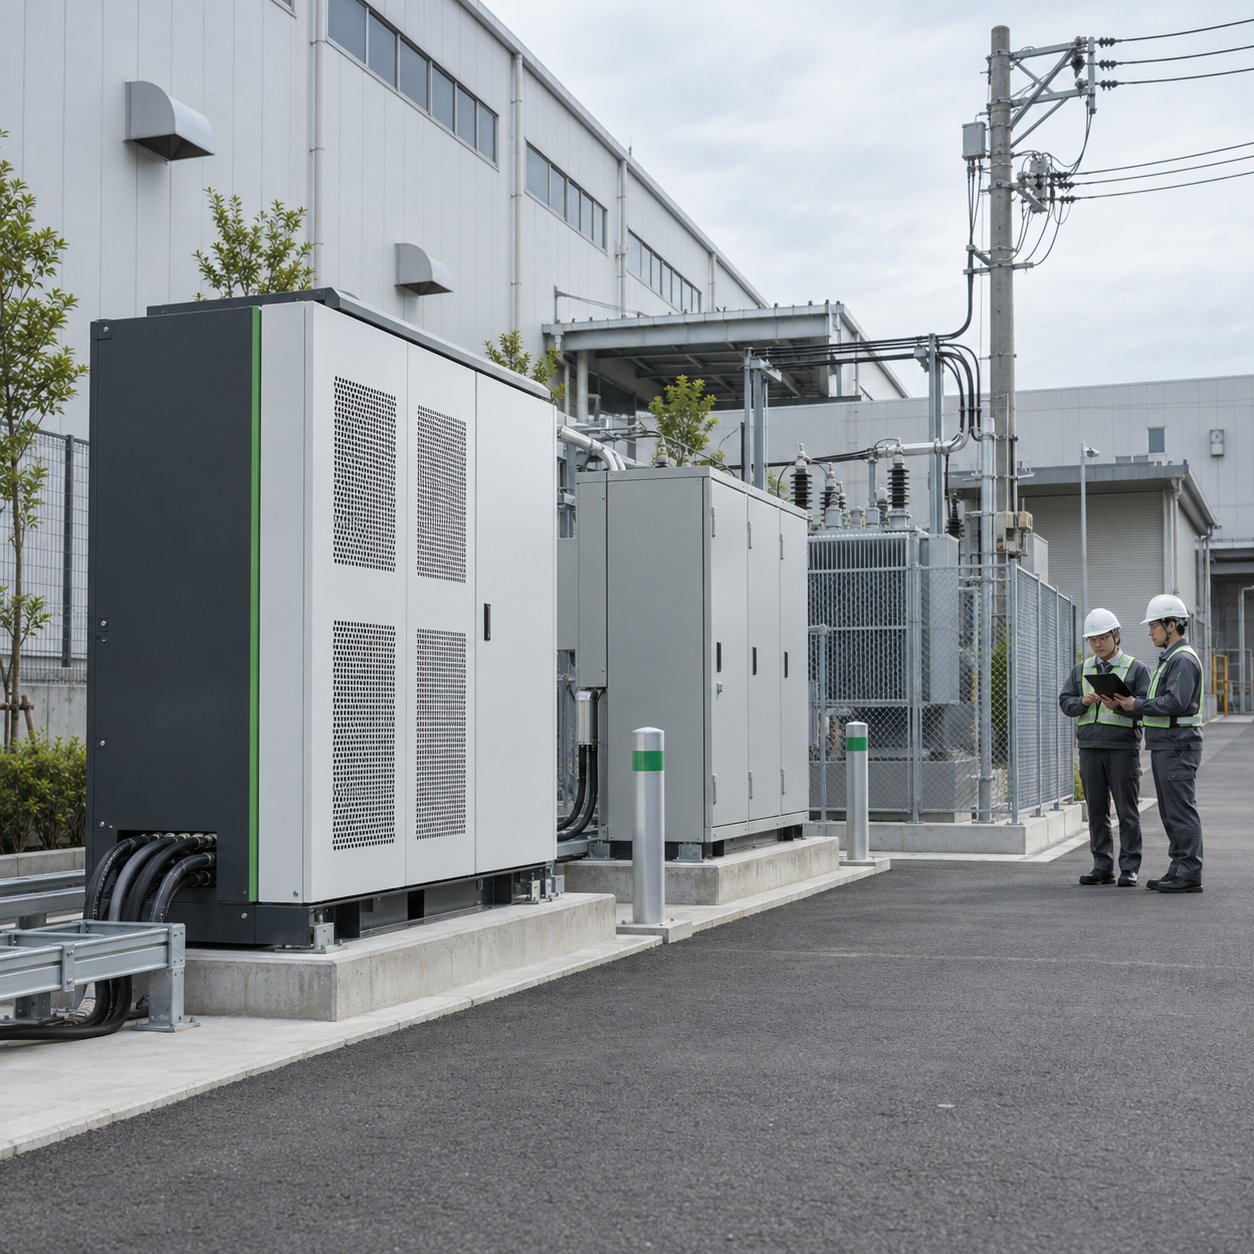
ESSA0100B-0215 can be screened first when measured demand reduction is at or below its 100 kW rated AC power and the multi-interval energy analysis fits the proposed dispatch. Treat 215.04 kWh as nominal capacity, not automatically available AC energy for every project condition.
Energon 261 and ESSC0500B-1075 should remain documentation-pending options in this article. A name that includes an energy-related number is not a substitute for traceable ratings, configuration details or engineering evidence. The relevant أنظمة تخزين الطاقة ذات الحالة الصلبة category and حالات الاستخدام can provide context, but they do not establish unstated model parameters.
Test the Proposed Dispatch Against the Worst Production Days
A credible commercial battery storage proposal should model the facility’s historical demand using the intended dispatch rules. The simulation should show original site import, battery discharge, battery recharge, resulting metered import, state of charge and intervals where the system cannot hold the target. It should test the highest-demand operating days as well as days containing two or more peak events.
The key question is not whether a demand cap can be achieved once. The key question is whether it can be achieved repeatedly through the planned production schedule while preserving sufficient state of charge and avoiding recharge-related peaks. If the analysis identifies a conflict, the answer may be greater battery energy, greater PCS power, a lower charging rate, a revised demand ceiling, changed production sequencing or coordinated load control.
Review results with the people responsible for production, receiving equipment and utility coordination. Buyers can learn more about the company through about MegSolid, but suitability for a Japanese high-voltage factory remains dependent on the offered equipment documentation, site electrical design, dispatch study and applicable local requirements.
Request a Preliminary Interval-Data Sizing Review
The most defensible decision sequence is to confirm the applicable demand rule, identify the measured peak interval, choose an import ceiling, calculate required kW and kWh, reserve a recharge window, and then test the proposed system against real production data. This avoids selecting commercial battery storage by a generic storage ratio while overlooking the PCS power and dispatch discipline required to control demand.
Submit a preliminary sizing-review request with:
- 30-minute interval load data
- Target demand ceiling and contract basis
- Single-line diagram and transformer information
- Production schedule across shifts
- Reverse-power-flow / no-export requirement
MegSolid can review the available system options against that duty, while the local EPC and electrical designer validate the 6.6 kV connection, protection and utility-facing requirements.
الأسئلة الشائعة
What is the difference between kW and kWh when sizing commercial battery storage for peak shaving?
kW is the discharge power needed to reduce facility demand at a given time. kWh is the energy needed to sustain that discharge for the required duration. Both must be evaluated against the measured demand intervals and planned operating reserve.
Is a 30-minute demand interval automatically the applicable rule for every Japanese factory?
No. The interval method, tariff treatment and contractual consequences must be confirmed for the specific utility contract, meter configuration and receiving-power arrangement.
Why must PCS power be assessed before battery capacity?
PCS power determines whether the system can supply the required AC demand reduction during a peak. A system with sufficient kWh but inadequate kW cannot fully cap the site import.
How is battery energy estimated for a 30-minute peak-shaving event?
Multiply the required discharge power by the required duration as an initial engineering calculation. Then account for project-specific losses, reserve policy, battery operating limits, auxiliary consumption and repeated peaks before selecting a system.
What is reverse power flow in a factory BESS project?
Reverse power flow occurs when BESS discharge exceeds facility load at the defined control point and power moves toward the grid. Its treatment depends on the interconnection agreement, metering, controls and protection design.
How should a recharge window be defined?
Define the available low-load period, maximum charge power, site-import headroom, required target state of charge and next expected peak. The recharge schedule should be simulated so it does not create another relevant demand peak.
What verified information is available for MegSolid ESSA0100B-0215?
The current MegSolid source files list 100 kW rated AC power, 215.04 kWh nominal capacity and a 672–850 V battery range for ESSA0100B-0215.
Can Energon 261 be recommended by assumed technical specifications?
No. Information is unavailable in the current MegSolid source files for a traceable model-specific technical comparison in this article. Obtain the exact datasheet and offered configuration before making a recommendation.
Can ESSC0500B-1075 be selected by its model name alone?
No. Information is unavailable in the current MegSolid source files for a traceable model-specific technical comparison in this article. Its power, energy, cooling, efficiency and grid-interface details should not be assumed.
How should a factory test a BESS against repeated demand peaks?
Run a dispatch simulation using historical interval-load data. Review resulting site import, battery state of charge, recharge commands and any intervals where the system cannot maintain the selected demand ceiling.
